Food Processing
EPOXY WALL
OUBOR
CHIPSY Factory
New production line & storage zones. Engineered for extreme thermal shock resistance.
New production line & storage zones. Engineered for extreme thermal shock resistance.
Drag the slider handle left and right to inspect the exact substrate condition before treatment versus the final engineered handover. Click either badge to view full screen.
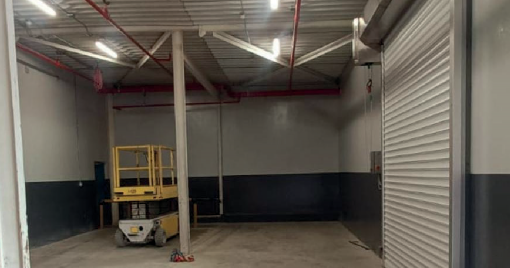 After • Final Handover
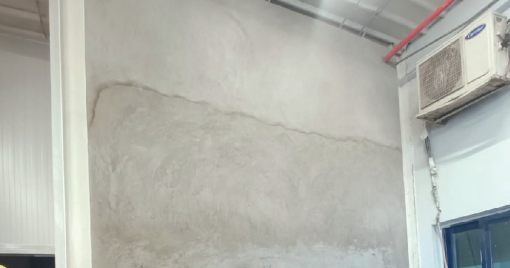 Before • Original State
The existing floor showed significant wear from thermal cycling and chemical exposure, compromising hygiene standards and operational efficiency.
The completed installation delivers exceptional performance under extreme conditions. Zero thermal cracks after 12 months, 99.9% bacteria resistance, and 40% improvement in cleaning efficiency.
Floor In adheres to strict ASTM substrate profiling, moisture barrier application, and conductive grounding protocols on every job site. Click any photo to view in full resolution.
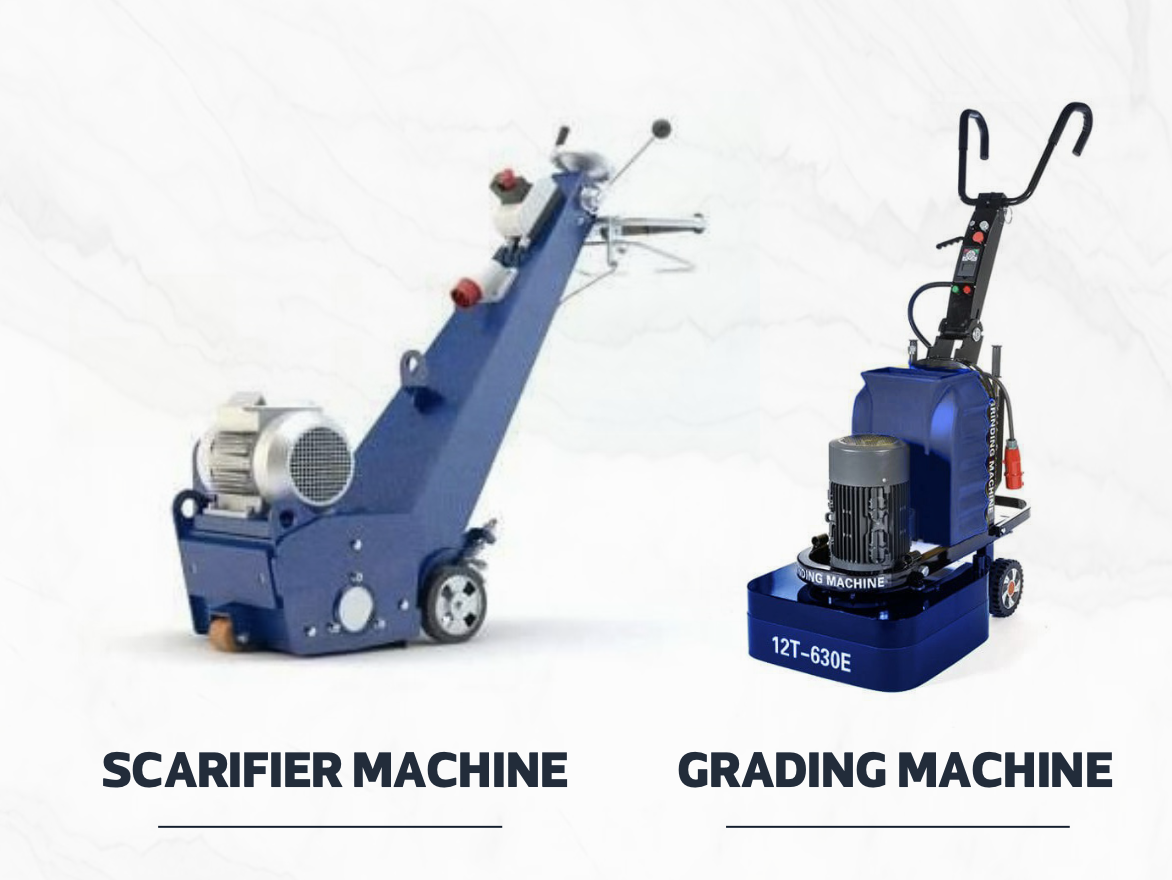
Surface preparation is one of the most important factors for the success of any epoxy floor system. Floor In uses the best and latest diamond grinding machines to achieve proper surface profile according to ICRI standards, ensuring maximum adhesion and system performance.
Surface moisture is measured before implementation using calibrated electronic hygrometers and ASTM F2170 compliance testing. For polyurethane systems, moisture levels must not exceed 4% to ensure proper curing and long-term adhesion. All readings are documented and verified.
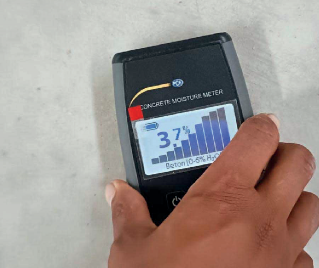
A specialized moisture-barrier epoxy primer was applied at 250 microns to strengthen the bond between concrete and the polyurethane system. The primer penetrates deeply into the substrate, creating a monolithic connection that prevents delamination under thermal stress and heavy loads.
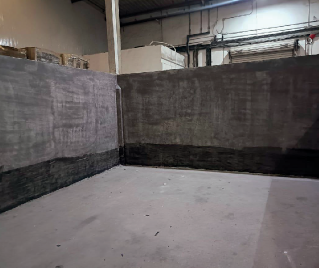
Epoxy-based leveling compound was applied to correct surface irregularities and fill expansion joints. This critical step ensures a perfectly flat substrate for the polyurethane coating, eliminating potential weak points and guaranteeing uniform thickness across the entire 12,000 sqm installation.
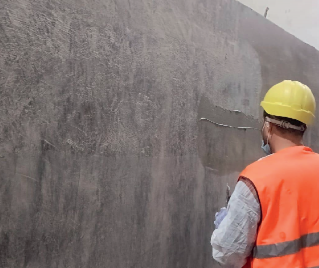
The final 6mm U-Crete polyurethane concrete layer was applied with integrated antimicrobial additives in industrial gold color. The system was enhanced with slip-resistant aggregates in wet zones while maintaining easy-clean properties. HACCP-certified for food contact surfaces.
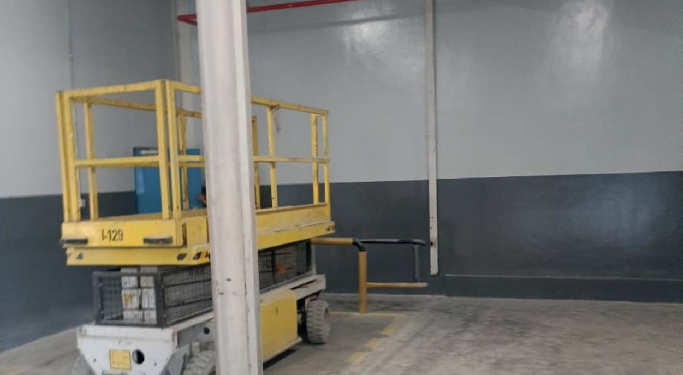
Our certified engineering consultants evaluate your substrate, measure ambient moisture, and engineer the optimal chemical-resistant epoxy or polyurethane system.