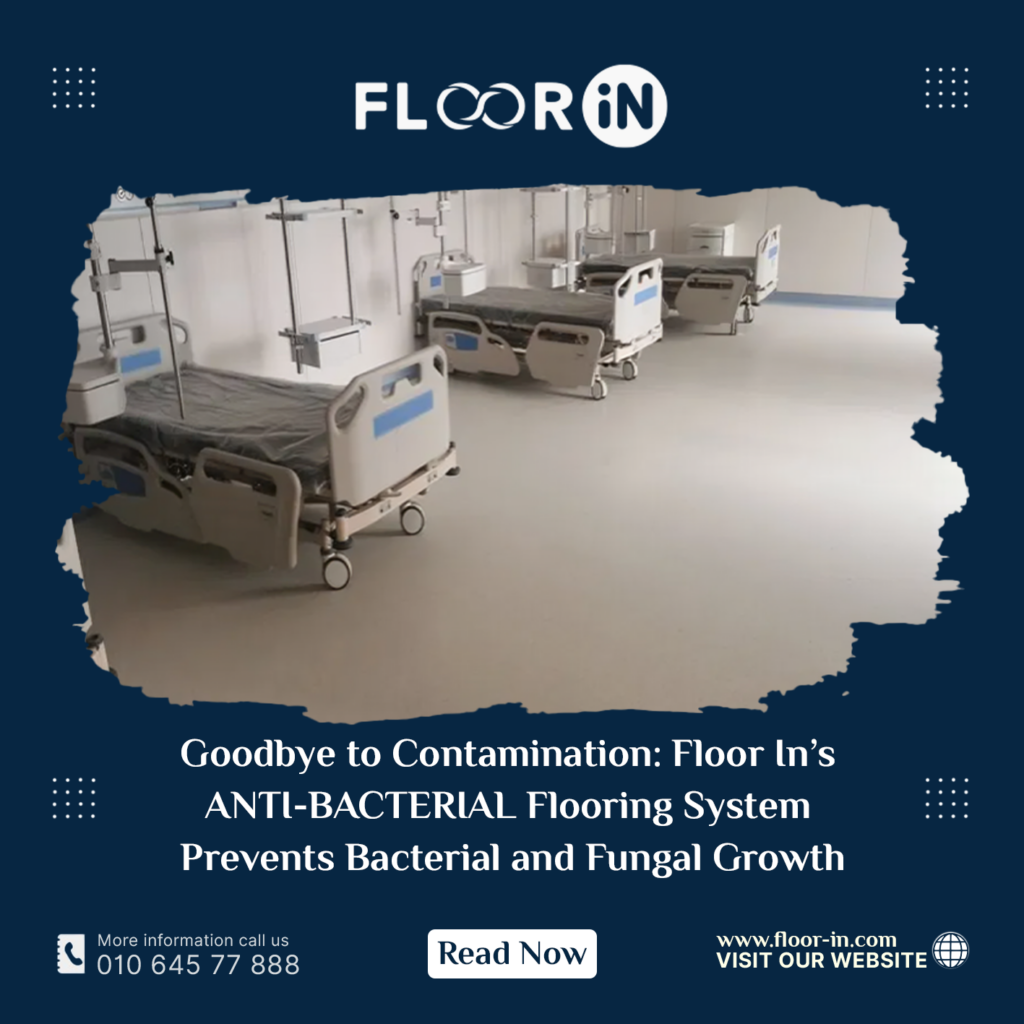
Goodbye to Contamination: Floor In’s ANTI-BACTERIAL Flooring System Prevents Bacterial and Fungal Growth In an era where hygiene and food and drug safety standards have become more stringent than ever, anti-bacterial flooring systems have emerged as a critical element in industrial and medical environments. Among the most innovative solutions that have redefined the industry, Floor In’s ANTI-BACTERIAL Flooring System stands out as a groundbreaking development in epoxy flooring—combining strength, cleanliness, and visual appeal.
What is Floor In’s ANTI-BACTERIAL Flooring System?
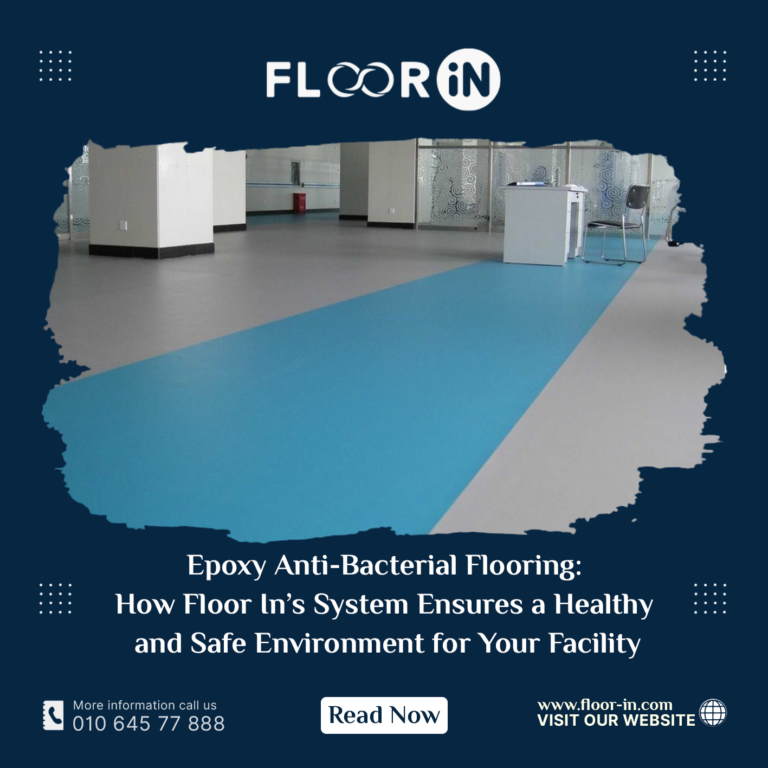
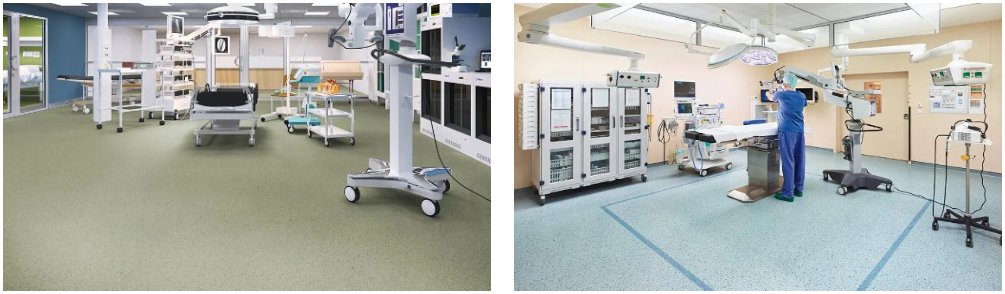
It is an advanced industrial flooring system based on epoxy that resists bacterial and fungal growth. It has been specifically engineered to meet the highest quality and safety standards in sensitive environments such as food factories, pharmaceutical plants, hospitals, operating rooms, and warehouses.
This system utilizes a unique formulation of Food Grade Epoxy and Pharmaceutical Epoxy, designed to prevent bacterial and fungal accumulation on surfaces. Its smooth, waterproof, and corrosion-resistant finish ensures easy cleaning and long-lasting hygiene.
Key Features of the ANTI-BACTERIAL Flooring System
-
High resistance to bacteria and fungi: Equipped with ANTI-BACTERIAL FLOOR technology that prevents microbial growth, ensuring a healthy and safe environment.
-
Complies with health and safety standards: Certified by regulatory bodies such as the Food Safety Authority and the Ministry of Health.
-
Smooth and easy-to-clean surface: Reduces the need for harsh chemicals and lowers maintenance costs.
-
Shock and abrasion resistance: Ideal for high-traffic industrial settings.
-
Temperature tolerance from 10°C to 80°C: Suitable for a wide range of applications.
-
Fast installation and time efficiency: Can be applied quickly without interrupting workflow.
-
Variety of colors and modern aesthetics: Meets both functional and design requirements.
Wide Range of Applications
The ANTI-BACTERIAL Flooring System from Floor In is used across various industries that demand superior hygiene standards:
-
Food Industries: Ensures a clean and safe production environment.
-
Pharmaceutical Industries: Where cleanliness and sterilization are non-negotiable.
-
Hospitals and Operating Rooms: Minimizes infection risks and supports patient safety.
-
Warehouses and Storage Facilities: Prevents mold and harmful bacterial spread.
-
Chemical Industries and Laboratories: Requires chemical-resistant, easy-to-clean flooring.
Technology Serving Cleanliness
One of the key components of this system is Self-Leveling Epoxy, which provides a seamless surface with no joints or gaps where bacteria can accumulate. The system also includes protective layers that resist abrasion and chemical damage, ensuring durability and long-term efficiency.
Why Choose Floor In?
Floor In is more than a flooring solutions provider—it is a trusted partner delivering cutting-edge technologies in anti-bacterial epoxy flooring. The company offers complete solutions from project design to professional installation and comprehensive after-sales support.
Unmatched Business Benefits
Choosing Floor In’s ANTI-BACTERIAL Epoxy Flooring System not only creates a hygienic environment but also offers significant long-term business advantages:
-
Reduced operational costs: Easier cleaning and maintenance reduce dependency on expensive sanitizing materials.
-
Enhanced productivity: A safe, bacteria-free surface minimizes contamination risks—vital for food and pharmaceutical industries.
-
Compliance with international standards: Helps facilities easily pass safety and quality inspections.
-
Long-term investment: Designed to last for years with minimal maintenance, ensuring cost savings over time.
Advanced Application Techniques
Floor In’s ANTI-BACTERIAL Flooring System employs modern installation technologies to ensure the best possible results:
-
Self-Leveling Epoxy: Provides even coverage and a flawless, smooth surface.
-
Multi-layer structure: Includes a primer layer, a protective layer, and a final anti-bacterial coating.
-
Flexible thickness (1–4 mm): Adjusted based on industrial activity and load capacity.
-
Fast and safe installation: Applied without disrupting operations, emitting no unpleasant odors or toxic fumes.
Comparison: Traditional Flooring vs. Floor In’s ANTI-BACTERIAL Flooring System
| Criteria | Traditional Flooring | Floor In ANTI-BACTERIAL System |
|---|---|---|
| Bacterial Resistance | Low | Very High |
| Compliance with Standards | Not Guaranteed | Certified |
| Lifespan | Average | Long-lasting |
| Ease of Cleaning | Difficult | Easy and Quick |
| Chemical Resistance | Weak | Strong |
| Aesthetics | Limited | Multi-colored & Elegant |
| Long-term Cost | High (due to maintenance) | Cost-effective |
A Cleaner Future Starts from the Floor Up
In an age where hygiene and safety standards define brand reputation, choosing the right flooring system is no longer a construction decision—it’s a strategic investment. Floor In’s ANTI-BACTERIAL Flooring System gives your facility a competitive edge, positioning your brand among those that invest in quality from the ground up.
Conclusion
Cleanliness is no longer optional—it’s a necessity mandated by regulations and consumer awareness. With Floor In’s ANTI-BACTERIAL Flooring System, you can combine hygiene, performance, and aesthetic appeal in a single integrated solution designed to meet today’s needs and tomorrow’s challenges.
Say goodbye to bacteria—and welcome a cleaner future!